News
Which garnet sand is better for waterjet cutting,80# or 120#
12/11/2026
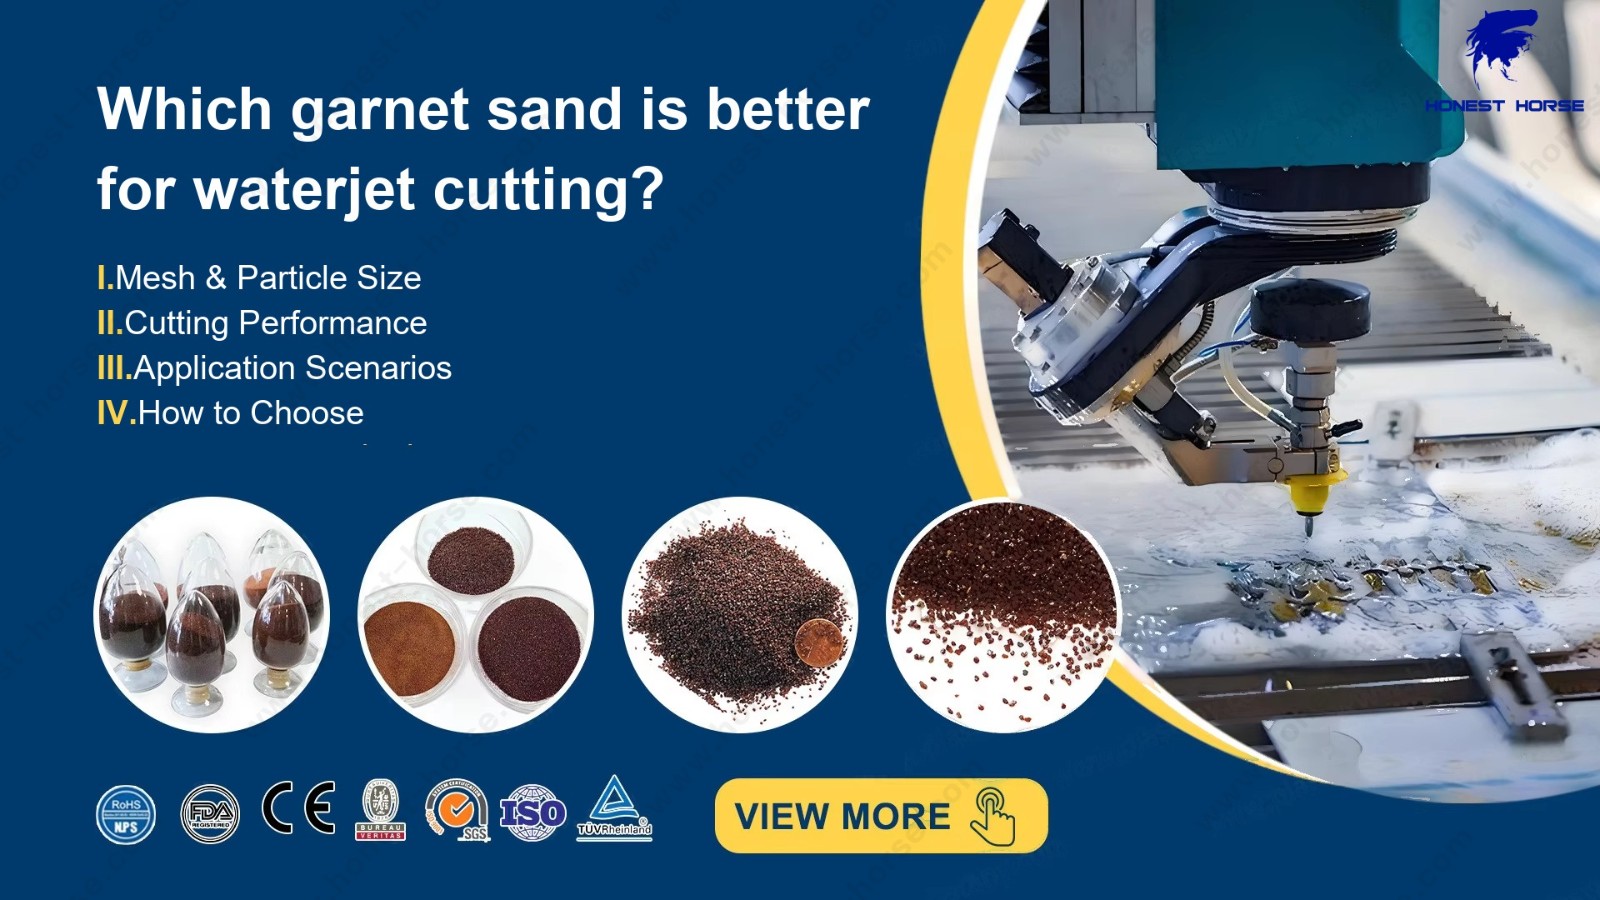
I. Mesh & Particle Size The rule is simple: the higher the mesh number, the finer the grit.
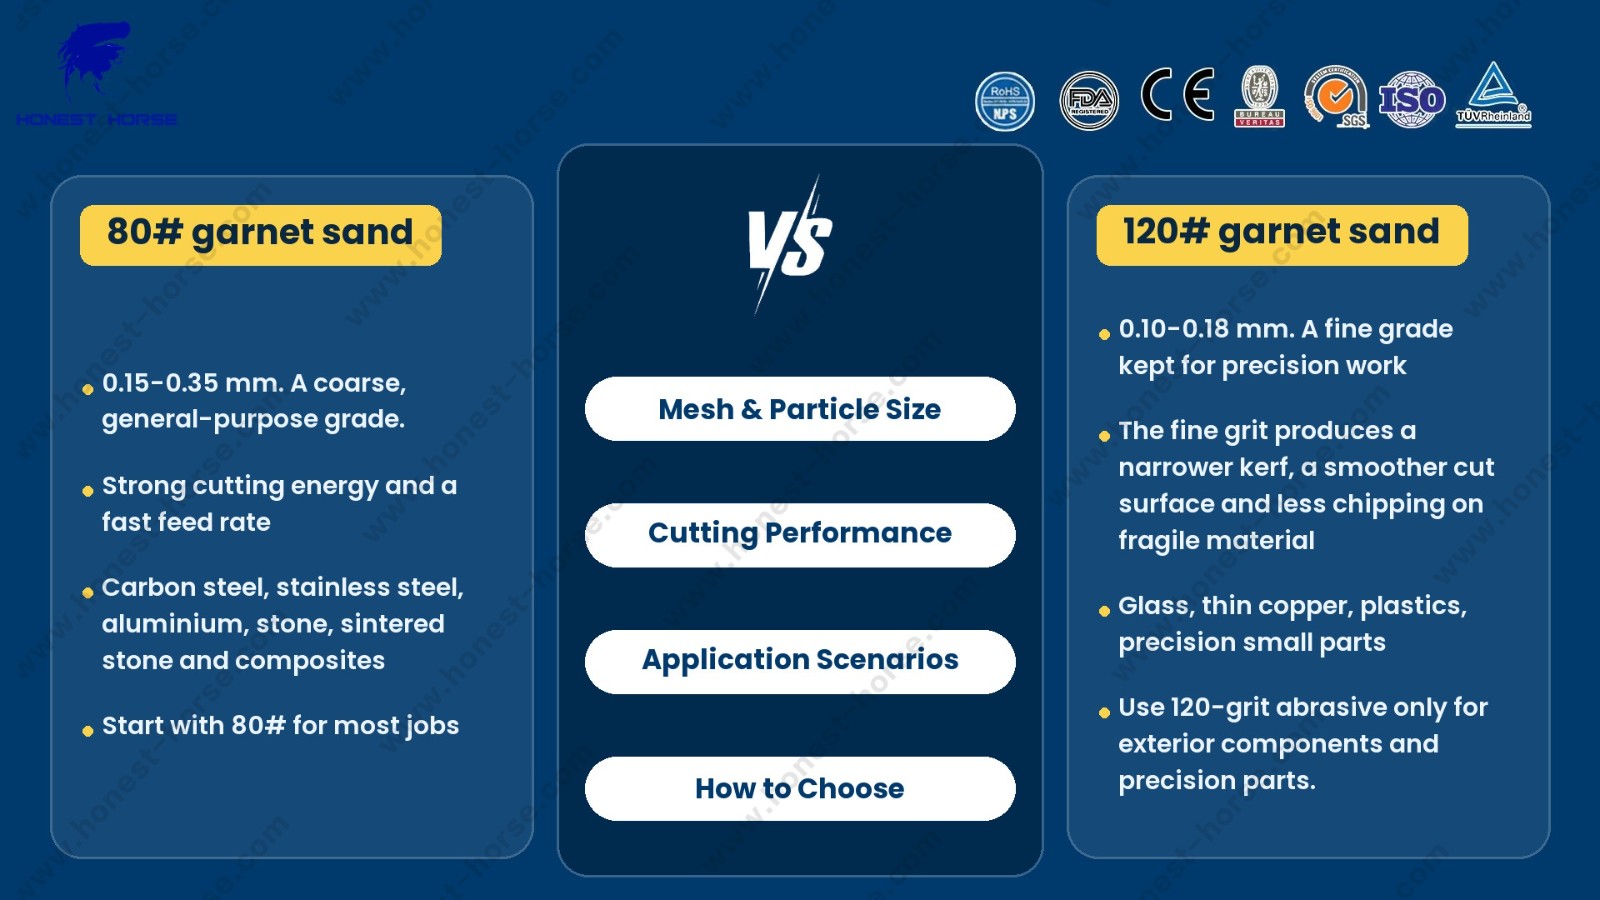
80#: 0.15-0.35 mm. A coarse, general-purpose grade.
120#: 0.10-0.18 mm. A fine grade kept for precision work.
II. Cutting Performance
80#: Strong cutting energy and a fast feed rate. It balances cutting speed with kerf quality and gives the best cost-performance of the common grades. It runs standard 0.76/1.02 mm focusing tubes without clogging, and handles both thin and thick plate. The cut surface is medium roughness, which meets most normal tolerance requirements.
120#: The fine grit produces a narrower kerf, a smoother cut surface and less chipping on fragile material. The trade-off is speed: it cuts about 30% slower than 80#. It also needs smaller 0.51/0.76 mm focusing tubes, consumes more abrasive for the same workload, and costs more per part. Thick, hard plate cuts poorly.
III. Application Scenarios
80#: Carbon steel, stainless steel, aluminium, stone, sintered stone and composites. Routine batch production and heavy stock cutting from 3 to 50 mm. This is the grade factories keep in stock and the most common choice in export orders.
120#: Glass, thin copper, plastics, precision small parts, cosmetic and exposed parts, and intricate fine patterns that demand a high surface finish.
IV. How to Choose
Start with 80# for most jobs: faster cutting, lower cost per part, fewer nozzle issues.
Move to 120# only when edge quality or fine detail matters more than speed, and the budget allows the extra abrasive consumption.
professional firm engaged in the research, development, sale, and service of Steel Shot, Steel Grit, sandblaster, sandblasting machine, garnet sand. We are located in Jinan with convenient transportation access. .
Quick links
Products Structure
Our Contacts
Building A.B.C ,Ouyadaguan Commercial Capital, No.67 Yangguang Xin Road, Shizhong District,Jinan City, Shandong Province, China
0086-531-82020205
+0086-15806668333
- Message
- WhatsApp
-
Whastapp
-

Message